How to Write a Product Inspection Checklist Your Inspector Can Actually Use
10 min read
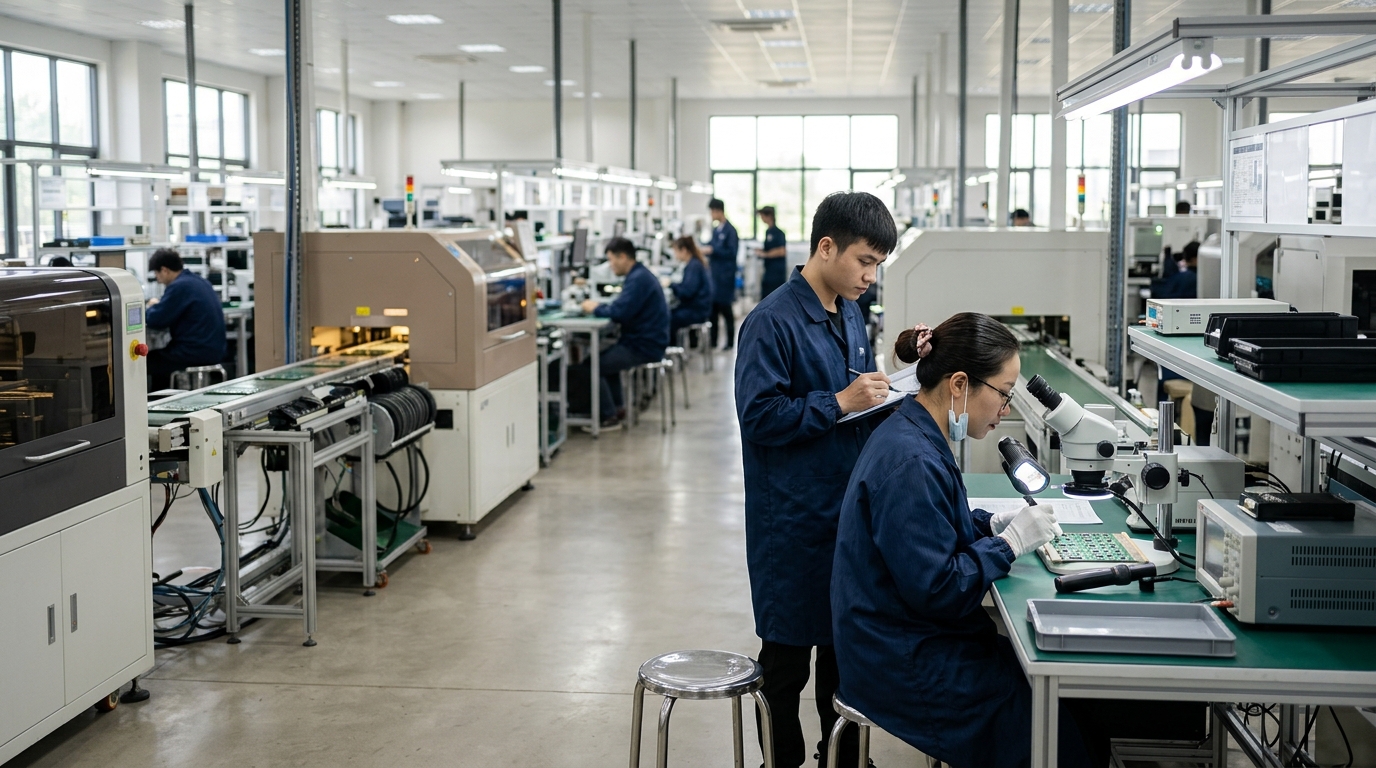
A product inspection checklist is the single document that converts your purchase order and approved sample into a set of instructions a third-party inspector can execute without calling you for clarification. When that document is well built, inspections are consistent across factories in China, Vietnam, Bangladesh, or Indonesia. When it is poorly built — or absent — inspectors default to general industry standards that may not reflect your specific product requirements, and defects slip through not because the inspector was careless, but because nobody defined what a defect was.
Most importers underestimate how much work goes into a usable checklist. A spec sheet lists what the product should be. A checklist turns that specification into a series of observable, measurable, pass/fail tests that a trained inspector can complete in a structured sequence during a pre-shipment inspection (PSI), an in-line inspection (ILI), or a pre-production inspection (PPI). The distinction matters because the same product will have different critical checkpoints at each stage.
This guide covers the architecture of a practical inspection checklist: the sections you need, the level of detail required in each, how to classify defects, and how to set sampling parameters using AQL. If you want to understand where checklist-driven inspections fit into a broader quality programme, start withthe Quality Control pillar guide, then return here for the operational detail.
The most common failure mode is not a missing section — it is ambiguity within sections that exist. Descriptions like "colour should match sample" or "stitching should be neat" give an inspector no actionable criterion. Does colour tolerance extend to a half-shade variation? What stitch count per centimetre defines neat? Without answers, inspectors make judgement calls, and those calls will vary across individuals, factories, and countries.
A second failure mode is conflating the approved sample with the checklist. The physical sample is a reference object; the checklist is the written standard. Factories can and do dispute inspection findings by claiming the inspector compared product to the wrong sample revision. A checklist that records the exact approved sample reference, SKU, and sign-off date closes that dispute before it starts.
Finally, checklists often omit packaging and labelling entirely, treating inspection as a product-only exercise. Retail buyers and importers regularly face chargebacks not because the product itself failed, but because a barcode was unreadable, a carton marking was wrong, or a required certification label was missing. Your checklist must cover the full commercial unit.
The Core Sections Every Product Inspection Checklist Needs
Regardless of product category — consumer goods, apparel, electronics, or hardgoods and furniture — a robust inspection checklist contains five functional sections. Each section should open with the relevant specification reference (drawing number, tech pack page, PO clause) so the inspector knows exactly where to verify the standard.
1. Quantity and Shipment Verification
Before any product testing begins, the inspector confirms that the correct quantity is present and ready for inspection. This section covers total carton count, units per carton, SKU breakdown against the packing list, and whether the production run is complete or partial. Partial production at the time of inspection is a common source of later non-conformances and should trigger an automatic hold or a note in the report.
2. Dimensional and Weight Tolerances
List every critical dimension from your approved drawing or tech pack, with the nominal value and the acceptable tolerance range. For a garment, this means key measurements by size. For a piece of furniture, it means overall dimensions, hole placements, and wall thicknesses. For an electronic enclosure, it means housing dimensions and connector positions. Weight tolerances matter for products where shipping costs are calculated by weight or where weight is a proxy for material content.
Specify the sample size for dimensional checks — it is rarely practical to measure every unit, so define whether you are measuring five units, ten units, or following a defined sub-sample protocol.
3. Appearance and Aesthetic Standards
This section is where most disputes originate, and it requires the most explicit language. Define defects in writing and, wherever possible, with reference photographs attached to the checklist. Classify each defect as critical, major, or minor using your own definitions rather than relying solely on general industry guidance.
Typical appearance checks include surface finish consistency, colour uniformity against the approved standard, print registration and legibility, seam alignment, hardware finish, and the absence of contamination such as stains, scratches, or mould marks. For apparel, add checks for pilling, snags, and fabric hand-feel against the approved swatch.
4. Functional and Safety Testing
List every function the product must perform and the method by which the inspector will verify it. For electronics, this means power-on testing, button and port functionality, and indicator light behaviour. For mechanical products, it includes articulation, load-bearing tests within safe limits, and assembly completeness. For apparel, it covers zipper operation, button attachment pull-force, and snap function.
Safety checks that can be performed on-site without laboratory equipment — such as checking that small parts are not present in a children's product, that sharp edges have been deburred, or that a cord length complies with a known standard — should be included here. Laboratory-dependent tests (flammability, chemical composition, electrical safety) belong in your pre-production testing protocol, not in the on-site checklist, though the checklist should confirm that test reports are present and in-date.
5. Packaging and Labelling Verification
This section is non-negotiable for any importer supplying a retail customer. Specify every element of the inner pack, master carton, and pallet (if applicable): carton dimensions, gross and net weight, drop-test requirements, barcode symbology and placement, required language on consumer packaging, country of origin statement, compliance marks (CE, FCC, RoHS, CPSC, or equivalent), and care/instruction labelling.
For retail-ready packaging, confirm shelf-ready dimensions, hang-hole placement, and whether the barcode scans correctly using the inspector's scanner. A single unreadable barcode on a retail floor triggers a markdown or a chargeback; catching it at origin costs a fraction of the alternative.
How to Set Defect Classifications and AQL Sampling Parameters
Defect classification is the backbone of a product inspection checklist. Most programmes use three levels:
| Classification | Definition | Typical AQL threshold |
|---|---|---|
| Critical | Risk of injury, regulatory non-compliance, or product unusability | 0 (zero tolerance) |
| Major | Functional failure or significant appearance defect likely to cause rejection or return | AQL 2.5 |
| Minor | Departure from spec that is unlikely to affect use or sale | AQL 4.0 |
AQL (Acceptable Quality Limit) is a statistical sampling standard — formally defined under ISO 2859-1 and its US equivalent ANSI/ASQ Z1.4 — that determines how many units to inspect from a batch and how many defects are permitted before the batch is rejected. AQL 2.5 for major defects is the most widely used threshold in consumer goods importing, though retail customers frequently require tighter levels.
Your checklist must state the AQL level for each defect classification, the inspection level (commonly General Inspection Level II), and the resulting sample size for the production quantity being inspected. Leaving this undefined means the inspector will apply a default that may not align with your retail customer's requirements.
Structuring the Checklist for Different Inspection Types
A product inspection checklist is not a single static document. The sections above cover a pre-shipment inspection comprehensively. For earlier inspection types, the scope narrows:
Pre-production inspection (PPI): Focus on raw material and component conformance — fabric weight, hardware finish, component dimensions, and approved material test reports. Functional and packaging sections are typically not yet applicable.
In-line inspection (ILI): Focus on work-in-progress quality at a defined production milestone, typically when 20-40% of the order is complete. Dimensional checks, appearance standards for the production stage, and process adherence are the primary scope. This is where catching a systematic defect — a consistent measurement deviation, a colour lot inconsistency — prevents it from running through the entire production batch.
Pre-shipment inspection (PSI): The full checklist applies. All five sections should be completed on a finished, packed, and production-representative sample.
If you are running inspections across multiple factories in different countries — a common situation for supply chain directors managing sourced production across China, Vietnam, and Bangladesh simultaneously — maintaining a single master checklist template and issuing factory-specific versions ensures that your results are comparable and that your supplier scorecard reflects a consistent standard.
How to Format the Checklist So the Report Is Audit-Ready
The output of an inspection is a photographic inspection report, and the structure of that report is determined by the structure of your checklist. Each checklist item should produce a corresponding line in the report: the specification, the finding, a measurement or observation, a pass/fail result, and where relevant, a photograph.
For a report to function as chargeback documentation — to defend a deduction claim or a warranty dispute — it must be traceable: inspector name and credentials, factory name and address, date and time, PO number, approved sample reference, and the specific checklist version used. Build these fields into the header of your checklist template so the inspector completes them at the start of every engagement.
If your organisation uses an ERP or PLM system, define the data fields in your checklist to match the import format your system accepts. This is especially relevant for procurement teams at larger organisations who need inspection results to flow into vendor scorecards without manual re-entry.
Common Checklist Gaps That Cause Avoidable Failures
Several omissions appear repeatedly in checklists that look complete but produce inconsistent results:
- No on-site reference sample specified. State whether the inspector should use a golden sample held at the factory, a sample held by your inspector's office, or a digital reference pack. Ambiguity here is exploited. - Missing tolerance for colour. Colour should be assessed against a physical approved swatch under a defined light source. Daylight, D65, and TL84 produce different colour appearances. Specify the light source. - No carton drop or compression test requirement. For sea freight shipments, carton integrity is a significant risk. Define whether a drop test is required and to what standard. - Absence of a rework policy. If the inspector finds a borderline result, what happens next? Your checklist should state the re-inspection conditions and who authorises a conditional release. - No escalation contact. The inspector should not be making commercial decisions. Name the person with go/no-go authority so the inspector's job is to report, not to negotiate.
Getting Your Checklist Into the Hands of the Right Inspector
A well-constructed product inspection checklist is only effective when the inspector reading it has the product knowledge and category experience to execute it correctly. An inspector experienced in hardgoods and furniture will approach a dimensional check differently from one whose background is apparel and textiles. When briefing a third-party QC provider, confirm that the assigned inspector has relevant category experience and has reviewed your checklist in advance — not on the morning of the inspection.
Sharing the checklist with the factory before inspection is a deliberate choice, not an oversight. Many importers share it openly on the basis that a factory that knows the standard will produce to it. Others prefer to withhold certain checks. The approach depends on your relationship with the supplier and your assessment of the risk of a coached inspection.
To see how a structured checklist integrates with a full inspection programme — from pre-production through to final release — exploreour Quality Control serviceand the broader inspection workflow it supports.
A product inspection checklist is not a one-time document — it is a living standard that should be updated each time a product specification changes, a retail customer adds a new requirement, or an inspection finds a defect category you had not previously defined. The factories and inspection teams that produce the most consistent results are almost always working from the most precisely written checklists.
Need eyes on the ground in Indonesia?
MTS verifies suppliers, audits factories and runs AQL-based inspections at every production milestone — reported in writing.
Related services
Related articles
Receive furniture sourcing insights across Asia.
One email per week. No spam.